


Releasing an internal thread when plastics injection molding is one of the challenges in designing and making injection molds. There are many reasons for this. On the one hand, there is a wide range of threaded products: caps of different sizes and various materials; tubular or stud-type products for length guidance; tight closing lids and much more.
Therefore, it was necessary to search for and create efficient principled and ready-made solutions for releasing the internal threads. Here we will present only some of them, for which KRASKO offers you ready-made solutions. We will focus on two main groups:
1. Releasing through unscrewing.
2. Releasing by opening inward (collapsing).
1. Releasing through unscrewing.
As the most successful and well unscrewing, the rotation through gears is considered, which is especially suitable for the multi-cavity forms. The motion is transmitted simultaneously and equally to each cavity, regardless of their number.
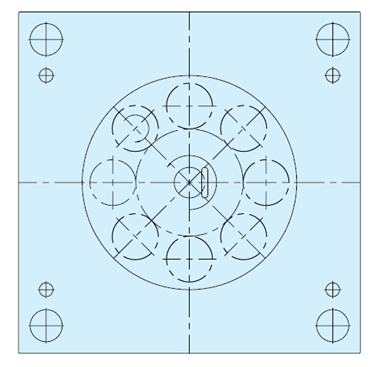
Unscrewing the rotary motion can be accomplished in several ways. We will look at some of them.
1.1. Unscrewing by screw pair - drive screw and nut.
1.2. The drive screw can be withdrawn at the main opening along the split surfise:

If preferred, the drive screw can also be withdrawn during ejection:

Elements for such a unscrewing drive can be found HERE
1.2. Drive by side-pull rack and pinion.
When the cavities are located in a row, it is preferable to turn the gears with a rack. For a very small number of revolutions (short stroke of the rack), a classic slider can be used. But a longer stroke is usually required, which can be accomplished with a hydraulic cylinder:

You can choose from the hydraulic cylinders we offer HERE
It is even more convenient to use the specially hydraulic cylinder with rack – hydraulic unscrewing device. It reduces overall dimensions and is easy to install and service:

You will find more about them HERE
2. Release by opening inward (collapse) .
When the product is in a large series, every tenth of a second in the injection cycle is important. Therefore, there are solutions that release the thread in the disposal process without waiting for unscrewing. Here are some of them:
2.1. Elastic collapsible cores - СС and ССМ

The standard CC hearts consist of a central core surrounded by a double spring-loaded head of sequentially collapsibles segments. The forward movement of the head releases the segments from the central stem support, segments 1 laterally release segments 2, and all segments retract to release the trimming of the article. The collapsible sleeve 3 is designed and constructed to collect the segments if for some reason they do not collapse on their own.

You will find more about them HERE
Collapsible cores mini CCM are designed for small diameters - below 10 mm. In order to save space, it is necessary to replace the segments 1 with three pieces of ribs (or knives) immovably connected to the central stem. Because they do not collapse, they form not undercuts, but smooth sections with a diameter equal to the outside diameter of the undercut. As the three-segment ring moves forward, they are simultaneously released from the center stem and blade support and retract, releasing the thread.

You can choose CCM hearts HERE
2.2. Profile Slide Collapsible Cores - Dovetail
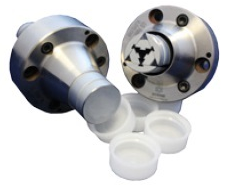
These collapsible cores are designed for reliable operation, connecting the release and stationary springs by means of a sliding dovetail assembly. The precise construction of the geometry ensures accuracy and durability of the mutual movement. A cooling channel is provided in the center.

DT-cores can be custom made or pre-selected for self-made molding. You can make your choice HERE
To prepare an offer for a collapsible cores, we need to send us:
- 3D model of the product in “step” format;
- Type of the Polymer material;
- Numbers of cavities;
KRASCO